
宁波贝琳达
BLD NINGBO PRANDELLI | ADVANCED FORGING SOLUTIONS
RED PUNCH FORGING LAB
CW617N (Leaded Brass) vs CW724R (Lead‑Free Brass) • Hot forging analysis on automatic hydraulic press | flashless forming | cycle 3.5s
📊 Machinability & Tool Wear Index
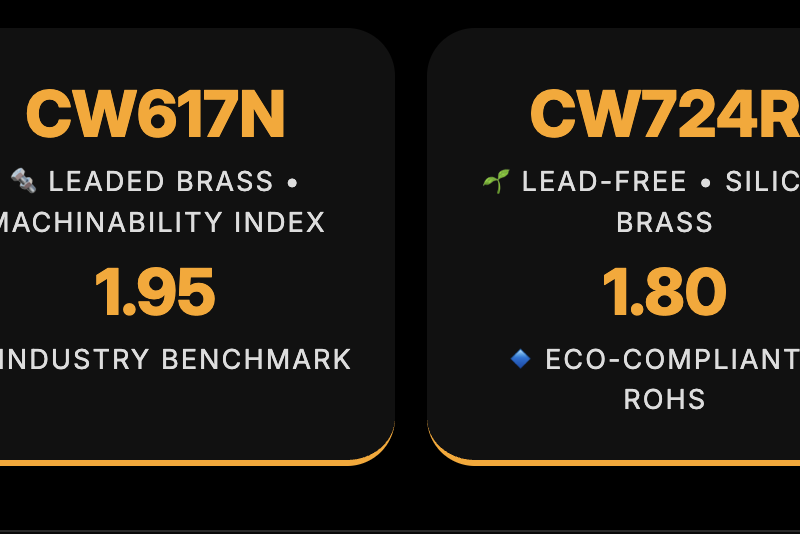
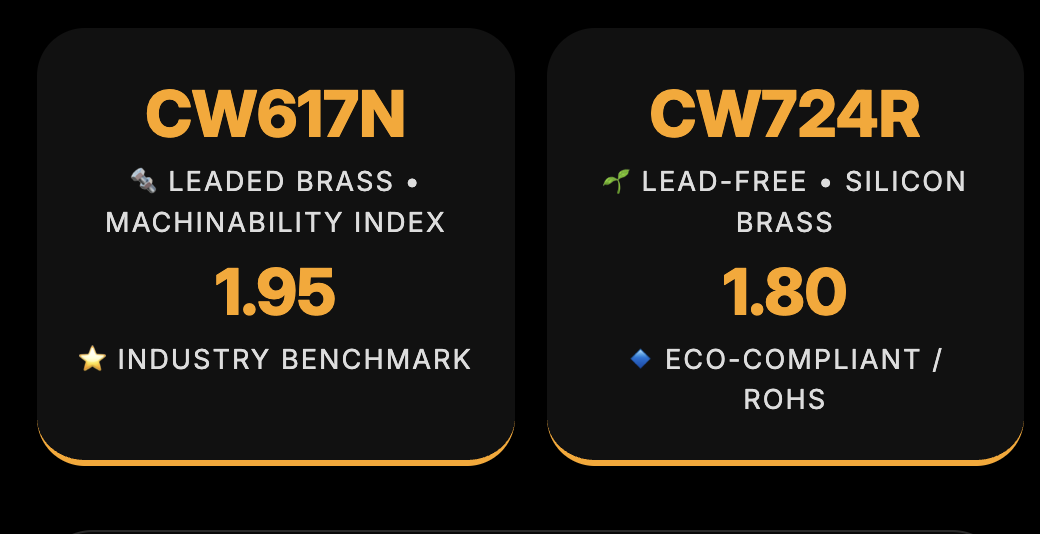
CW617N leaded brass offers superior machinability (1.95) vs CW724R (1.80). Lead acts as internal lubricant, reducing tool friction. For CW724R, carbide tooling is recommended due to higher abrasion from silicon-phosphorus phases.
💪 Relative Forming Pressure (kN)
CW724R (lead‑free) requires approx. 22% higher forming pressure to fill complex cavities due to lower hot ductility. RED PUNCH models (ZG250/4G60: 2500kN main cylinder) are well suited, but high tonnage versions recommended for CW724R multi‑cavity tees/elbows.
🛠️ Projected Die Life (Thousands of parts)
RED PUNCH 20‑head adjustable graphite spraying extends die life. CW617N yields up to 40% longer tool life. For CW724R, more frequent lubrication cycles + high‑quality DLC or carbide molds are advised.
🔥 Process Efficiency & Rejection Rate
Infrared temperature sensing + automatic rejection of underheated billets ensures quality. CW617N shows lower risk of surface cracks. CW724R demands strict 650‑750°C window to prevent subsurface deformation twinning.
📋 Metallurgical & Process Parameters
| Property / Parameter | CW617N (Leaded Brass) | CW724R (Lead‑Free Brass) | RED PUNCH Advantage |
|---|---|---|---|
| 🔹 Hot forging temp range | 650°C – 750°C | 660°C – 760°C | Medium‑frequency furnace / gas heating ± precise control |
| 💧 Material flow in multi‑cavity | Excellent (Pb lubricates) | Good, needs higher pressure & lubrication cycles | 4 independent hydraulic punches, 4G60 series (4 side cylinders) |
| ⚡ Flashless forging potential | Optimal, consistent filling | Very good but requires accurate blank volume | Flashless design → raw material saving up to 1.2 mm per cut |
| 🔧 Punch wear rate | Low (standard tool steel) | Higher (abrasive Si-rich phases) | Punch displacement control (Balluff) + 1/100 sec core accuracy |
| 🌿 Environmental compliance | Lead restricted in potable water (EU/US) | Full RoHS, EPA, drinking water approvals | Sustainable solution with natural gas heating optional |
| 🏭 Typical applications | Plumbing fittings, gas valves, high‑pressure brass components | Lead‑free faucets, eco water meters, medical gas fittings | HVAC, sanitary components, refrigeration, fire protection |
🧩 Graphic Insight: Multi‑Directional Forging Principle
4 hydraulic cylinders with independent speed control, acceleration via proportional valves. For CW617N, smooth multiport cavity filling. For CW724R, pressure boost & controlled sequence avoid cold shuts. The 1/100s core extraction accuracy ensures complex geometries like elbows and tees.
Heating uniformity – intermediate frequency furnace (or optional gas) with PID zones. CW724R needs narrow tolerance (±10°C) to minimize deformation twinning. The machine’s optical pyrometer auto‑ejects billets out of range.
📈 Economic & Environmental Impact
⚡ Material savings per cut (flashless)
Flashless forging reduces brass consumption by ~1.2mm per blank compared to traditional trimming. Over 1 million parts → up to 1800 kg of brass saved. Benefit equally for CW617N and CW724R.
🌿 Energy consumption (natural gas furnace)
Optional gas recovery combustion reduces gas usage by ~25% compared to conventional systems. RED PUNCH press + smart heating = green manufacturing with low emission.
